Heat-shrink tubes mostly use EVA and polyolefins as base materials and are expanded and set after irradiation or chemical crosslinking; they must be flame retardant while maintaining shrink ratio, elasticity and insulation performance. Coated red phosphorus has high flame-retardant efficiency and requires a low dosage, making it suitable for dark/black wire harness heat-shrink tubes, but in such thin-wall extrusion compounds, if several details are not handled well, yellowing, screen clogging, exudation and inconsistent flame retardancy can occur.
The first is moisture protection and safety. Although coated red phosphorus is more stable than ordinary red phosphorus, once the surface absorbs moisture or the coating is damaged, it will still slowly oxidize and release phosphine, causing odors and reddish-yellow discoloration during processing. The raw material must be stored sealed in a cool, dry place and used up as soon as possible after opening; avoid high humidity in the production environment; give priority to multi-layer continuously coated grades with a high ignition point and extremely low phosphine release to reduce safety hazards at the source. The second is temperature control and oxidation prevention. The extrusion temperature for EVA heat-shrink tubes is usually in the range of 160–190°C; avoid local overheating of the barrel and long residence time. Excessive temperature will oxidize and yellow the red phosphorus surface and generate acidic substances, affecting appearance and weakening flame retardancy; this is also one of the causes of the yellow flocculent material that many customers see at the screen. The third is dispersion and filtration. Red phosphorus has high specific gravity and readily agglomerates, so a compatibilizer or coupling agent is needed to disperse it uniformly; the screen mesh size must match the filtration process, and screens must be cleaned regularly to prevent undispersed particles and free coating material from accumulating on the screen surface. The fourth is the color limitation: red phosphorus systems can only be used for black, dark brown and other dark tubes, not light-colored or transparent products; confirm the color requirements of the product before selecting a grade.
In actual formulations, coated red phosphorus is often compounded synergistically with magnesium hydroxide and phosphorus-nitrogen components to reduce the red phosphorus dosage while balancing flame-retardant rating, tensile strength and shrinkage performance; also ensure compliance with RoHS, REACH and electrical insulation-related requirements, and conduct a small-scale trial before production to confirm self-extinguishing after flame removal, shrink ratio and appearance.
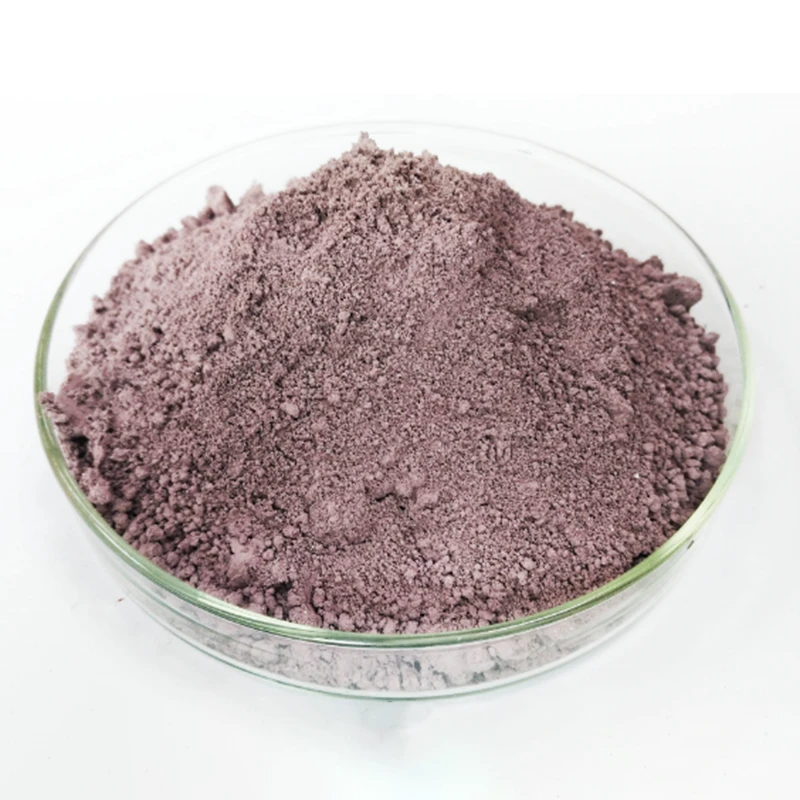
Dongguan Hongtaiji Flame Retardant Materials' multi-layer coated red phosphorus has high active content and uniform particle size, an ignition point of ≥300°C and phosphine release below 1PPM; it is suitable for EVA and polyolefin heat-shrink tube compounds, supports free samples and formulation adjustment, and the entire series complies with RoHS and REACH standards.